
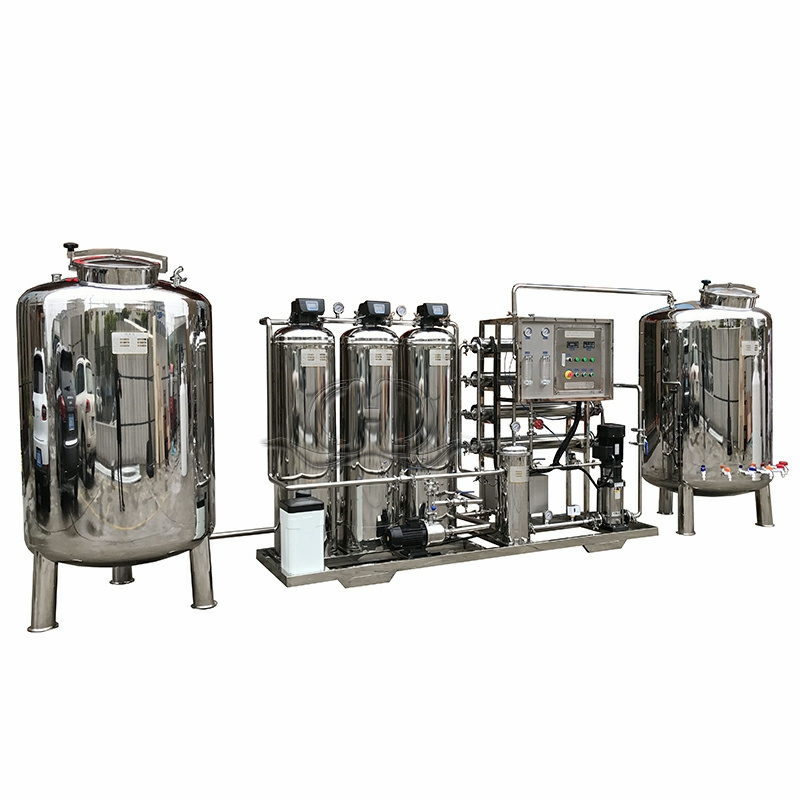
Wenzhou Haideneng Environmental Protection Equipment & Technology Co., Ltd., a leader in the water treatment industry, has recently introduced its cutting-edge 500 liters per hour (Lph) reverse osmosis (RO) plant, setting new standards for efficiency, reliability, and innovation in water purification technology. This latest offering underscores the company’s commitment to transforming water resources worldwide and providing clean, safe, and sustainable water solutions that meet the evolving needs of communities and industries alike.
### Company Overview
Established as a pioneering force in environmental protection and water treatment, Wenzhou Haideneng Environmental Protection Equipment & Technology Co., Ltd. has built a strong reputation for its robust and forward-thinking approach to water purification systems. Headquartered in Wenzhou, the company combines advanced technology with environmentally responsible practices to deliver systems designed for a broad range of applications—residential, commercial, and industrial.
The company's mission, “to transform the water around us into the water you need around the world,” truly captures its vision. This commitment drives continuous innovation that helps mitigate water scarcity, improve water quality, and ensure sustainable water management across diverse regions and industries.
### The 500 Lph RO Plant: Innovation and Efficiency
The newly launched 500 Lph RO plant is designed to efficiently convert raw or brackish water into high-quality potable water. Utilizing reverse osmosis technology, the system removes up to 99% of dissolved salts, organic impurities, bacteria, and other contaminants, ensuring the output meets stringent health and safety standards.
The plant’s capacity of 500 liters per hour makes it an ideal solution for small to medium-scale operations. Whether for commercial facilities, community water supply, small-scale manufacturing units, or remote areas with limited water access, this RO plant offers a reliable and cost-effective water treatment solution.
Several key features and benefits distinguish this 500 Lph RO plant:
- **High Filtration Efficiency:** The RO membranes are designed for optimal water passage while blocking contaminants, achieving excellent purification results with minimal waste.
- **Energy-Efficient Operation:** Leveraging advanced components and an intelligent control system, the plant minimizes energy consumption, lowering operational costs and environmental impact.
- **User-Friendly Interface:** The system includes a simple control panel with real-time monitoring, making it easy to operate and maintain, even in locations with limited technical expertise.
- **Durable and Compact Design:** Engineered for longevity, the plant’s modular design and corrosion-resistant materials ensure stability and ease of installation across different sites.
- **Customizable Configurations:** Depending on water quality and usage requirements, the system can be tailored with pre-treatment units and post-treatment options to maximize performance.
### Addressing Global Water Challenges
Access to clean water remains one of the most pressing global challenges. According to the United Nations, over 2 billion people lack safely managed drinking water services. Industrialization, population growth, climate change, and contamination of natural resources have intensified the need for scalable, effective water purification technologies.
Wenzhou Haideneng’s 500 Lph RO plant targets these issues by providing a practical solution that can be deployed in both urban and rural settings. For communities facing water contamination from salinity, heavy metals, or microbial pollutants, this technology offers a pathway to safe drinking water, crucial for health and wellbeing.
In addition, industries such as food and beverage production, pharmaceuticals, textiles, and electronics—which require high-purity water in their manufacturing processes—can benefit from these systems. Ensuring the availability of purified water can improve production quality while adhering to environmental regulations and sustainability goals.
### Commitment to Sustainability and Environmental Protection
Sustainability lies at the core of Wenzhou Haideneng’s development philosophy. By emphasizing water reuse and conservation, the company’s technologies help reduce freshwater extraction, minimize wastewater discharge, and lower chemical usage.
The 500 Lph RO plant integrates eco-friendly features such as waste water recovery and low chemical dependency. These enhancements contribute to reducing environmental footprints while maintaining superior performance. Additionally, the company’s ongoing research and development efforts focus on further improving energy efficiency and membrane life cycle.
### Supporting Customers Globally
Wenzhou Haideneng Environmental Protection Equipment & Technology Co., Ltd. also prides itself on delivering comprehensive customer support—from initial consultation and system design, through installation, training, and after-sales service. By understanding local water conditions and customer requirements, the company ensures each RO plant performs optimally and meets regulatory standards.
With a growing installation base across different countries, the company has demonstrated its ability to adapt solutions for diverse climates, water qualities, and application scales.
### Future Outlook
Looking ahead, Wenzhou Haideneng aims to expand its product portfolio further, continuously incorporating innovative technologies such as smart sensors, AI-based monitoring, and renewable energy integration to enhance system intelligence and sustainability.
The introduction of the 500 Lph RO plant marks another milestone in the company’s journey to lead the water treatment sector by providing intelligent, effective, and eco-conscious water purification solutions.
### Conclusion
As global demand for clean and safe water intensifies, Wenzhou Haideneng Environmental Protection Equipment & Technology Co., Ltd.’s launch of the 500 Lph reverse osmosis plant represents a significant advancement in accessible and reliable water treatment technology. This system, embodying efficiency, sustainability, and user-centric design, reaffirms the company’s mission to transform the water around us into the water people need around the world.
For communities, businesses, and industries seeking dependable solutions to water contamination and scarcity, the new RO plant delivers practical benefits and contributes to a healthier, more sustainable future.
---
**About Wenzhou Haideneng Environmental Protection Equipment & Technology Co., Ltd.**
Wenzhou Haideneng Environmental Protection Equipment & Technology Co., Ltd. is a leading provider of reliable and innovative water treatment systems. The company is dedicated to delivering advanced solutions that ensure clean, safe, and sustainable water worldwide, transforming the water around us into the water you need.